FAI, 8D, PFMEA, traceability, and release records
Quality Assurance for PCB Assembly When Reports Must Prove the Build
Quality assurance for PCB assembly is valuable only when it connects the released files, inspection evidence, failure mode, and corrective action into one auditable record. YourPCB supports FAI, 8D, and PFMEA-driven review for OEM programs where a finished PCBA needs more than a pass sticker before the next lot repeats.

Where FAI, 8D, and PFMEA Fit in PCBA Quality
FAI, 8D, and PFMEA answer different buyer questions in a PCB assembly program. A first article inspection checks whether the first produced assembly matches the released files. An 8D report explains containment and corrective action after a defect. A failure mode and effects analysis asks which process risks should be controlled before the next lot repeats.
The strongest quality file links those documents to the real PCBA route: solder paste printing, pick-and-place setup, reflow, through-hole soldering, AOI, X-ray, ICT, programming, and functional test. Standards context from IPC electronics standards and ISO 9000 quality management helps define the language, and regulated device teams often compare report discipline against the FDA's Quality System Regulation. The buyer still needs numeric pass-fail limits and product-specific evidence.
Scope and Capability Boundaries
FAI Release Evidence
First article inspection ties the first acceptable PCBA to the exact BOM, XY data, assembly drawing, workmanship criteria, inspection images.
8D Corrective Action
Structured 8D reporting separates containment, root cause, permanent action, verification.
PFMEA Review
Process failure mode review maps likely SMT, soldering, inspection, test, and handling risks before repeat production hides them inside normal yield loss.
Traceability Records
Lot records connect board revision, BOM version, solder paste lot, component date codes, AOI or X-ray evidence.
Inspection Stack Planning
AOI, X-ray, ICT, flying probe, visual inspection, and functional test are assigned by failure mode instead of added as generic quality wording after quoting.
Supplier Quality Handoff
Reports are written so OEM engineering, purchasing, and supplier quality teams can make decisions without translating factory shorthand after a problem occurs.
Honest Fit Guidance
This service is strongest when the build has real evidence to inspect: released files, photos, test data, failed units, lot numbers, or a proposed process route. It is not a substitute for product safety certification, regulatory approval, or root-cause certainty when no boards, records, or defect samples are available. If the work also needs procurement and manufacturing ownership, start with turnkey electronics manufacturing and add quality reporting to that build plan.
Real SMT First Article Inspection (FAI) Report
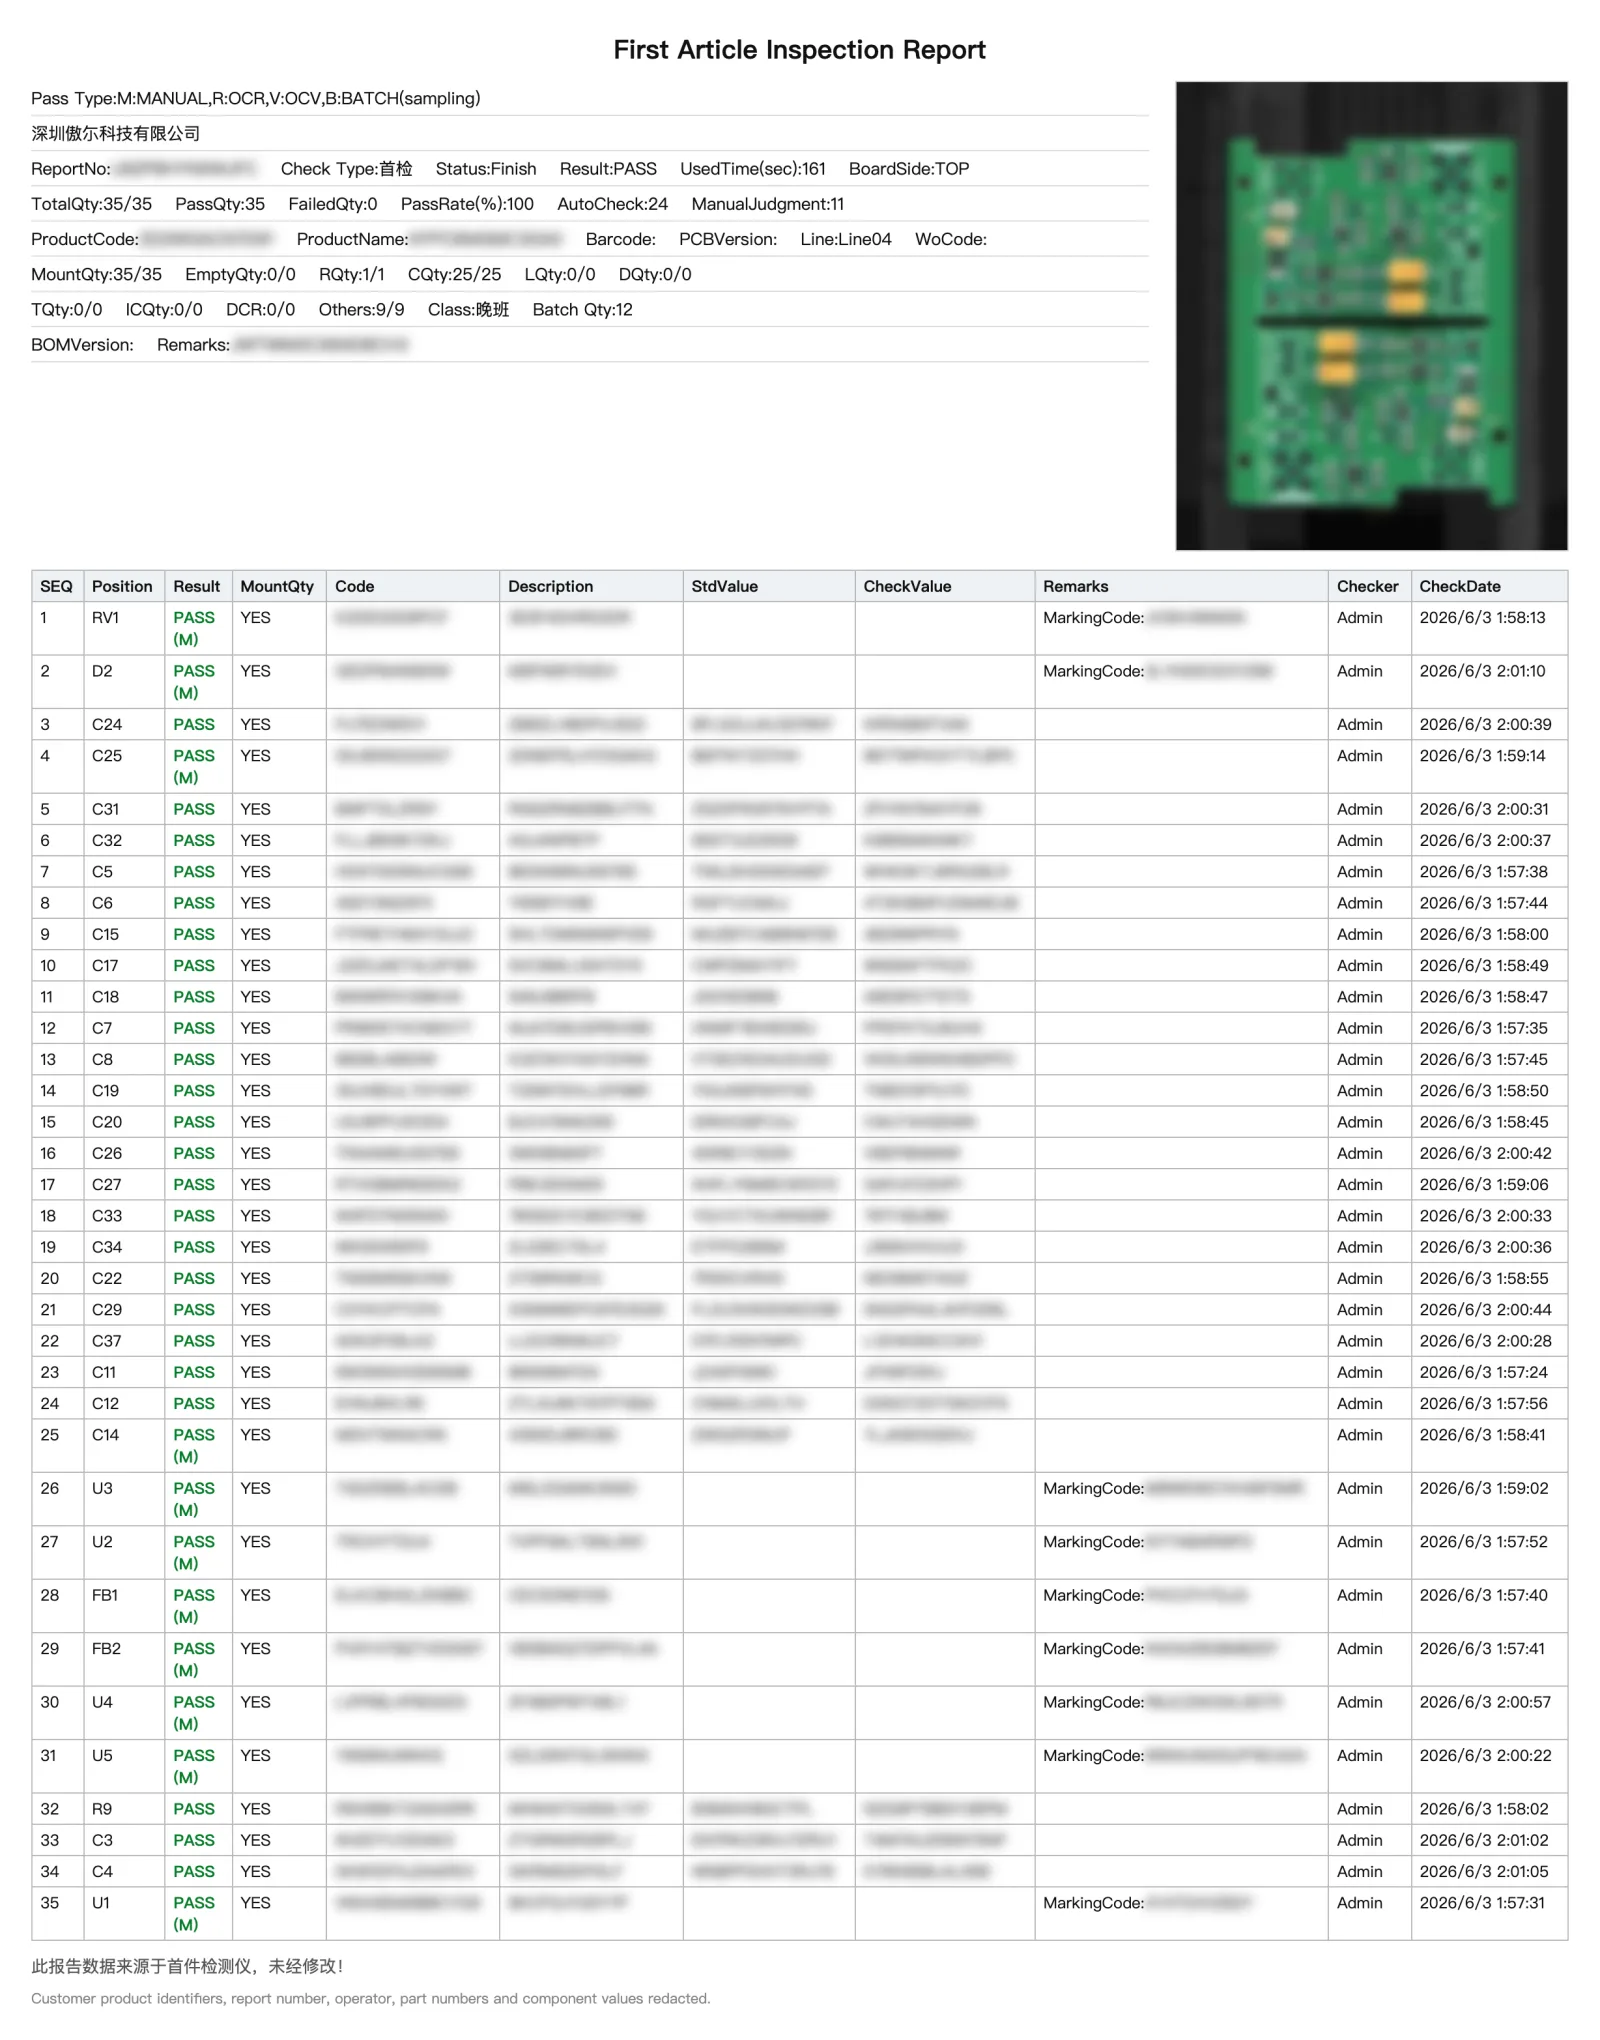
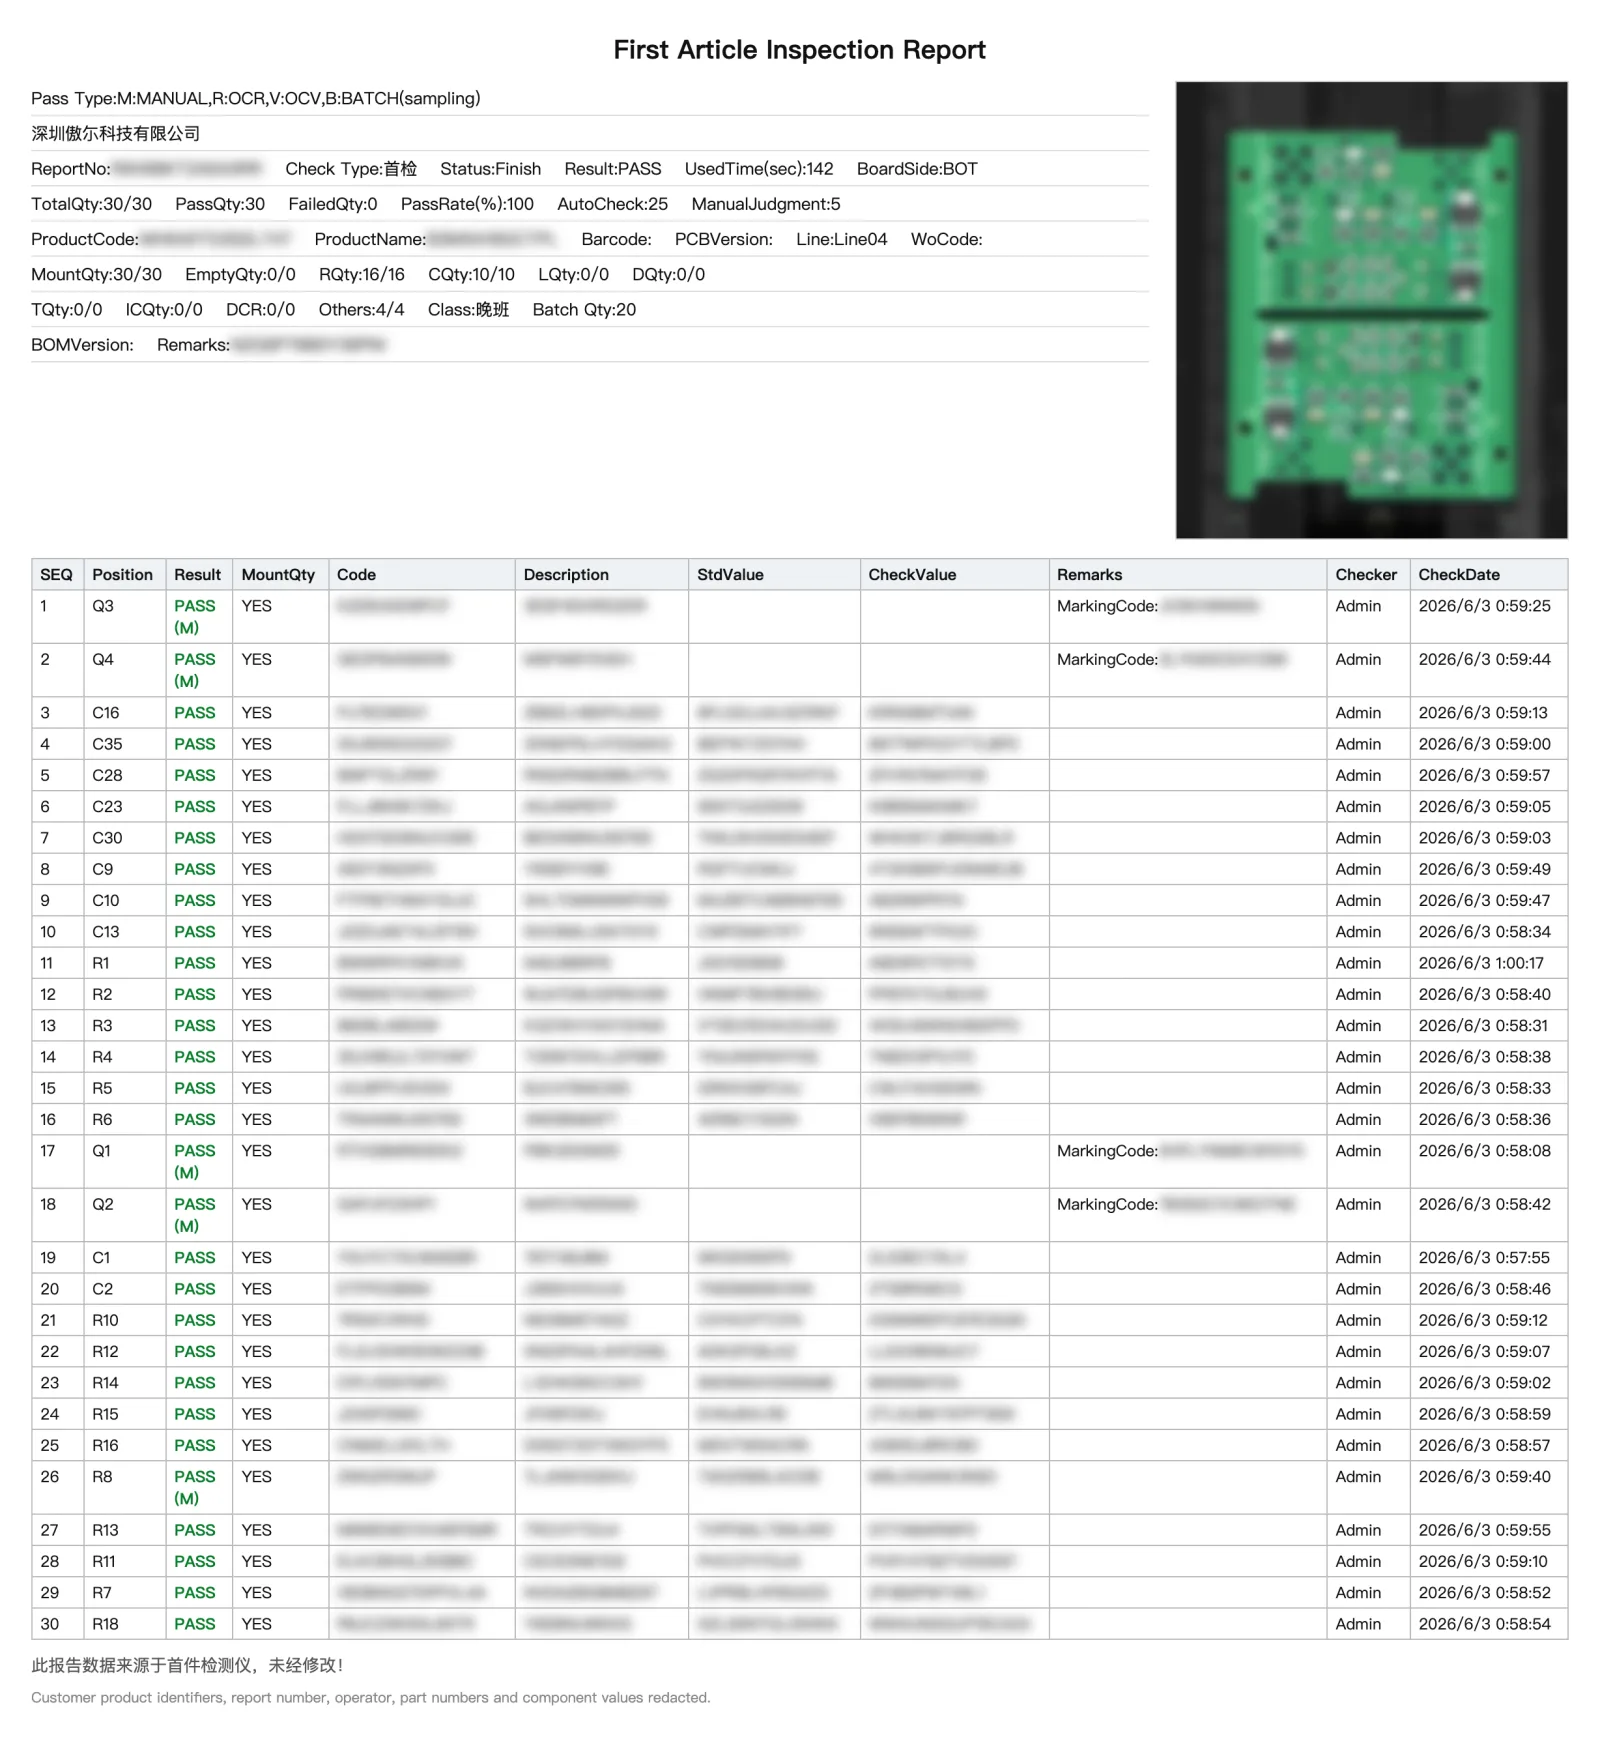
First article inspection is how a wrong reel on a feeder, or a part that does not match the BOM, gets caught before the batch runs. The two reports below come from SMT Line04 at Shenzhen Aoer Technology (深圳傲尔科技有限公司), a sister company in our group, on 3 June 2026: one first-article check for the top side and one for the bottom side, each run on a first-article tester. Customer product identifiers, the report number, part numbers and component values are redacted; every other field and every pass/fail verdict is exactly as the tester printed it.
| Side | Placements checked | Result | Auto / manual judgment | Inspection time |
|---|---|---|---|---|
| Top | 35 | 35/35 PASS | 24 auto · 11 manual | 161 s |
| Bottom | 30 | 30/30 PASS | 25 auto · 5 manual | 142 s |
What the report records
- One line per reference designator (RefDes): whether the part was placed (MountQty) and the verdict.
- For resistors and capacitors, the BOM standard value (StdValue) next to the measured value (CheckValue); these values are redacted in the images.
- References without a nominal value (U, D, FB, Q: ICs, diodes, ferrite beads, transistors) are checked by the inspector against the part marking and marked PASS (M).
- Every verdict carries the inspector and a time stamp to the second, so you can see who checked the first article and when.
This report covers placement and component values. If you need FAI with dimensional, visual, electrical or functional results, say so in your quote request and we will agree the scope and format with you.
Technical Signals Buyers Should Define
| Best-fit programs | Prototype, pilot, bridge, and controlled low-volume PCBA or electronic assembly builds |
|---|---|
| Core documents | FAI report, 8D report, PFMEA notes, control-plan inputs, inspection release records |
| Standards references | IPC-A-610 workmanship, ISO 9001:2015 QMS logic, IATF 16949-style corrective action thinking |
| Typical evidence | AOI images, X-ray findings, test logs, build traveler notes, lot and revision traceability |
| Useful triggers | New product launch, ECO release, supplier transfer, repeat defect, critical component substitution |
| Report inputs | Gerber or ODB++, BOM, XY data, assembly drawing, pass-fail limits, defect photos, test data |
| Out of scope | Regulatory certification, product safety approval, or guaranteed root cause without physical evidence |
These signals keep the quote conversation anchored in evidence. A supplier can prepare a useful FAI or 8D only when the acceptance rule is measurable, the affected lot is bounded, and the report owner knows which process step can prevent the next escape.
Comparison: Which Quality Document Solves Which Problem?
| Document | Best use | Evidence | Risk if skipped |
|---|---|---|---|
| FAI | First build approval before continuing a pilot or repeat run | Ballooned checks, BOM match, placement review, photos, inspection signoff | Wrong setup can repeat across every board in the lot |
| 8D | Customer-visible defect, repeat escape, line stop, or field complaint | Containment boundary, root cause, corrective action, verification record | Rework hides the symptom while the process failure remains |
| PFMEA | NPI, automotive-style controls, or process changes before repeat production | Failure modes, severity, occurrence, detection controls, action owner | Known risks stay informal and do not become inspection gates |
| Control plan | Stable production where checks must repeat by lot or operation | Process step, characteristic, sample size, reaction plan, record type | Operators inspect inconsistently when volume or staff changes |
| Traceability log | Medical, industrial, automotive, or field-serviceable assemblies | Revision, lot, date code, test result, rework status, shipment release | A defect investigation cannot isolate affected units quickly |
The practical decision is timing. Use FAI before production repeats, use 8D after a defect proves the current control failed, and use PFMEA when the team needs to prevent known risks before the next release. Combining all three on every order creates paperwork; applying the right one at the right gate creates control.

Factory Scenario: Pilot Lot With a Repeated Polarity Escape
A representative pilot scenario is a 180-piece industrial control PCBA where the first 20 units pass basic power-on test, but 6 later units fail because one polarized diode was rotated during a feeder change. The useful response is not only rework. The quality file should identify the suspect serial range, contain all boards built after the setup change, inspect the same reference designator across the lot, and verify the corrected feeder and AOI rule before production resumes.
In that scenario, FAI confirms the corrected first acceptable board, the 8D report captures containment and root cause, and the PFMEA update adds polarity-sensitive feeder verification as a control point. The result is a repeatable lesson: a failure found on six boards becomes a new release gate for the next 500-board order instead of a memory held by one operator.
How the Quality Review Workflow Runs
Define the Quality Question
We first separate launch approval, recurring defect, supplier transfer, and process-risk questions because FAI, 8D, and PFMEA solve different problems.
Collect Build and Defect Evidence
Engineering reviews Gerbers, BOMs, XY data, drawings, traveler notes, AOI or X-ray images, test logs, photos, and affected serial or lot numbers.
Map Failure Mode to Control
Each risk is tied to the control that can catch it earliest: feeder verification, stencil print control, reflow profiling, AOI, X-ray, ICT, or functional test.
Issue Report and Containment
The report identifies accepted units, suspect material, required rework, inspection evidence, immediate containment, and the owner of each corrective action.
Verify Prevention on the Next Lot
Corrective action is only useful when the next lot proves the change worked, so repeat builds carry the updated inspection gate or PFMEA action forward.
What to Send for a Useful Report
- Gerber or ODB++ files, drill data, and assembly drawing
- BOM with manufacturer part numbers and approved alternates
- XY placement data, revision notes, and polarity callouts
- Inspection requirements for AOI, X-ray, ICT, or visual checks
- Functional test procedure with numeric pass-fail limits
- Failed samples, photos, test logs, and affected serial numbers
- Lot size, date range, shipment records, and containment status
- Known ECOs, substitutions, feeder changes, or process changes
- Customer-specific formats for FAI, 8D, PFMEA, or control plan
- Required response deadline and owner for report approval
If the issue is mainly electrical coverage, pair this review with ICT testing service or a product-specific functional test plan. If the issue starts before assembly, use custom circuit board review to clean up fabrication and DFM risks first.
FAQ: FAI, 8D, and PFMEA for PCB Assembly
What is included in PCB assembly quality assurance support?
PCB assembly quality assurance support includes first article inspection, build-record review, AOI or X-ray evidence where needed, traceability checks, nonconformance handling, 8D corrective action, and PFMEA updates for repeat defects. The normal input package is Gerber or ODB++ data, BOM, XY placement, assembly drawing, revision notes, and the buyer's acceptance criteria. YourPCB uses IPC-A-610 workmanship language as a reference point, then ties the report to the exact board revision, lot quantity, inspection gate, and pass-fail rule.
I need 200 PCBAs for a pilot lot. Should I request FAI before the full run?
Yes, a 200-piece pilot lot is a good fit for first article inspection because one wrong feeder slot, polarity callout, or firmware label can affect the whole batch. A practical FAI freezes the first acceptable board with BOM line checks, placement verification, solder-joint review, critical measurements, and photos before the line continues. For dense SMT assemblies with 0402 passives, 0.5 mm pitch ICs, or BGA packages, FAI should be paired with AOI data and X-ray review where hidden joints carry risk.
When does an 8D report make sense for an electronics manufacturing issue?
An 8D report makes sense when a defect has reached the buyer, repeats across lots, stops production, or exposes a systemic process weakness. The report should identify containment, root cause, corrective action, verification, and prevention rather than only saying the board was reworked. In PCB assembly, useful 8D evidence may include suspect lot boundaries, feeder setup records, stencil or reflow data, AOI images, X-ray findings, operator checkpoints, and a PFMEA or control-plan change that prevents recurrence.
How is PFMEA different from a first article inspection report?
PFMEA is a risk-planning document, while a first article inspection report is evidence from a specific build. PFMEA asks what can go wrong in the process, how severe the failure would be, how often it might happen, and how well current controls detect it. FAI proves whether the first produced assembly matches the released files and inspection criteria. For a stable PCBA program, the two should connect: FAI findings feed PFMEA updates when the first build reveals a real process risk.
What files should I send if I need FAI, 8D, or PFMEA support?
Send the released Gerber or ODB++ package, BOM with manufacturer part numbers, XY placement file, assembly drawing, schematic or critical-net notes, quality requirements, target quantity, and any known defect evidence. For an 8D request, include photos, failing serial numbers, test logs, field symptoms, and the date range of affected shipments. For PFMEA review, include the proposed process route, special characteristics, inspection gates, and customer-specific requirements so risk ratings reflect the real build.
Can quality reports replace functional testing on PCB assemblies?
No. Quality reports document what was inspected, measured, contained, or corrected, but they do not prove product behavior unless functional test is part of the release plan. A board can pass visual inspection and still fail firmware boot, current draw, RF performance, or system communication. For higher-risk PCB assembly, use FAI and inspection records to prove build conformity, then use ICT or functional test to prove electrical behavior against numeric pass-fail limits.
How do I verify a supplier can support automotive-style quality expectations?
Ask for a real sample of the supplier's FAI record, 8D format, PFMEA update path, traceability fields, and revision-control process before placing a critical order. Automotive-style programs often expect IATF 16949 thinking, control plans, documented containment, and evidence that corrective actions are verified across future lots. Even when the product is not automotive, this review shows whether the supplier treats quality as a release system or as a final visual check.
Related Services
ICT Testing Service
Use ICT when quality evidence must include repeatable net-level fault detection and faster debug for stable PCB assembly revisions.
Medical PCB Assembly
Use this path when inspection records, lot traceability, and risk-based release planning matter for medical electronic assemblies.
Automotive PCB Manufacturing
Use this path when FAI, 8D, PFMEA, traceability, and change control need to align with automotive-style expectations.
Electronic Assembly Services
Use this path when the quality plan must cover PCBAs, harness interfaces, programming, labels, and final electromechanical release.
Custom PCB Assembly
Use this path for drawing-controlled PCB assemblies where variant logic, firmware, and product-specific checks drive release risk.
Need FAI, 8D, or PFMEA Support for a PCB Assembly Build?
Send the released files, lot history, defect evidence, and reporting requirement. We will help define whether the next step should be first article approval, containment, corrective action, or process-risk prevention.
Start a Quality Review
Backed by our group's Shenzhen SMT factory (Shenzhen Ao'er)